GRP Tank Manufacturers: 8 Criteria to Check Before You Choose a Supplier
Choosing the type of tank is the easy part. If you already know what you need — vertical or horizontal, buried or above ground, what capacity, which resin — you have solved half the problem; and if you are not there yet, we work through that decision step by step in our guide to GRP tanks: types, advantages and industrial applications. The other half, the part almost nobody explains, is who you buy it from.
What actually determines the service life of a GRP tank and cannot be seen on the finished vessel: the corrosion barrier and the joints.
Contact moulding, filament winding and dual laminate: three processes and three very different kinds of manufacturer.
Eight objective criteria for assessing a GRP tank manufacturer, with the exact questions to put to them.
The standards a credible quotation should cite: BS EN 13121, ASME RTP-1, ASTM D3299 and D4097, BS 4994 and PE(S)R.
Acceptance testing you are entitled to demand: Barcol hardness, thickness, glass content, tightness and acoustic emission.
The documentation pack your manufacturer should hand over, and five common procurement mistakes.
Choosing the type of tank is the easy part. If you already know what you need — vertical or horizontal, buried or above ground, what capacity, which resin — you have solved half the problem; and if you are not there yet, we work through that decision step by step in our guide to GRP tanks: types, advantages and industrial applications. The other half, the part almost nobody explains, is who you buy it from.
That half matters more than it appears, for one very specific reason: two GRP tanks built to the same drawing, to the same capacity and in the same resin can differ by fifteen years in service life. The difference lies in how the inner layer was laminated, in how the base and the top have been joined to the shell, in whether the resin has fully cured, and in whether anyone verified all of that before the vessel left the works. None of it is visible on the finished tank, and none of it can be put right afterwards.
A note on terminology before we start. In the UK the material is normally called GRP (glass-reinforced plastic); in North America and much of Asia the same product is sold as FRP (fibre-reinforced plastic). They are the same thing, and you will meet both acronyms in datasheets and tender documents.
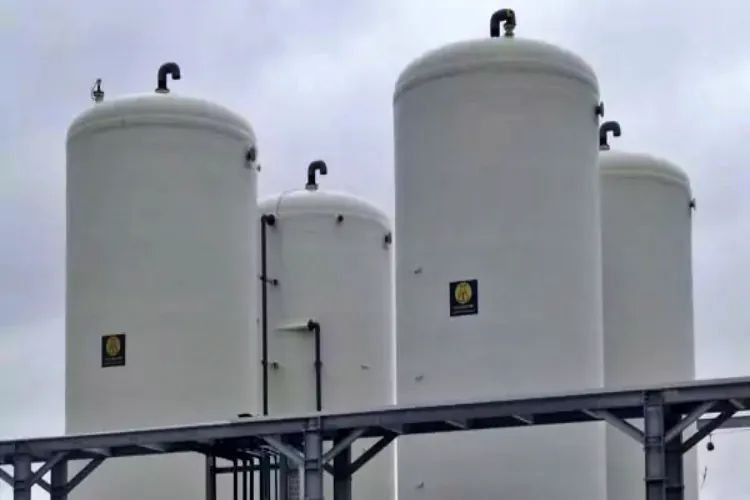
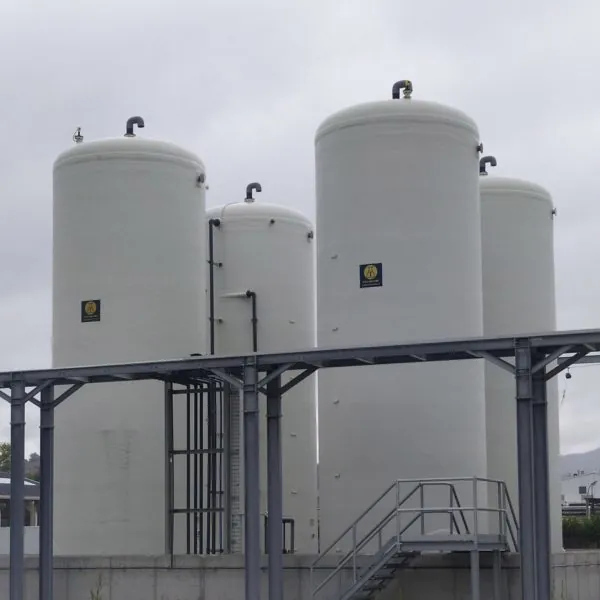
Tecnium, a Spanish manufacturer of GRP and thermoplastic tanks since 1957, builds tanks, vessels, reactors and stacks of up to 200,000 litres for the chemical industry, water treatment, surface treatment and fertiliser production. This guide sets out the criteria we apply internally, and which you can use to assess any quotation — ours or a competitor’s.
Why the manufacturer matters more than the quoted price
What you cannot see on a finished tank: the corrosion barrier
A GRP laminate is not a homogeneous material. It is a layered structure in which each layer does a different job, and the one that decides the tank’s service life is precisely the one you cannot inspect: the internal corrosion barrier, the only surface in permanent contact with the stored product.
That barrier consists of a surfacing veil — C-glass or synthetic — followed by two layers of chopped strand mat, all of it at a very high resin content, typically 70 to 90 per cent, against the 30 to 40 per cent of the structural laminate behind it. The result is a resin-rich skin roughly 2.5 mm thick whose purpose is not mechanical strength but keeping the chemical away from the glass fibre. Once the fluid reaches the glass, the failure mechanism runs away with itself: the fibre wicks the liquid inwards, the attack progresses through the laminate and delamination follows. At that point there is no repair, only replacement.
Here is the commercial problem underneath all this: thinning the corrosion barrier or specifying a cheaper veil cuts cost appreciably and changes nothing whatsoever about how the tank looks. The buyer does not notice it at handover; they notice it three years later. Which is why the first question to any manufacturer should be how many millimetres of corrosion barrier they are offering, with which veil, in which resin, and on what basis.
How the base and the top are joined to the shell
If the corrosion barrier is the first hidden factor, the second — and in practice the one that separates a good manufacturer from a poor one — is how the base and the top are joined to the cylindrical shell. A GRP tank is not built in one piece: the shell, the base and the top are produced separately and then joined with an overlay laminate applied across the seam.
That joint overlay carries two demands at once. First, it is the most highly stressed area of the tank: the base-to-shell joint takes the full hydrostatic load plus the bending moments generated by the change in geometry, and it is where cracking appears when the overlay has been made too narrow or too thin. Second — and this is what tends to get overlooked — the corrosion barrier has to be rebuilt continuously across the seam on the inside. If the internal overlay is omitted, or laid up without a veil and without the same resin content as the rest of the barrier, the seam is left as a line of structural laminate directly exposed to the product. The rest of the tank can be immaculate and it will still fail there.
The questions to ask are specific: whether the overlay is applied internally as well as externally, what width and thickness it has relative to the shell thickness, whether the surfaces were abraded before lay-up — without preparation there is no bond — and to which standard the joint has been designed. Both BS EN 13121-3 and ASME RTP-1 cover the design of these joints; a quotation that says nothing about them is leaving out the single place where most tanks fail. It is also worth checking the knuckle radius at the base-to-shell transition: a generous radius spreads the stress, a sharp corner concentrates it.
Contact moulding, filament winding and dual laminate
Not every GRP tank manufacturer does the same thing, even though they all sell «fibreglass tanks». There are three processes, and it is worth knowing which one your supplier genuinely commands:
Contact moulding (hand lay-up): the layers are applied by hand onto the mould. It allows complex geometries, local reinforcement, manways, nozzles and rectangular tanks, and it is the process that demands the most craft: quality depends directly on the laminator. It is the basis of ASTM D4097, BS EN 13121 and ASME RTP-1.
Filament winding: continuous fibre is wound mechanically at a controlled angle. It produces very consistent laminates with higher glass content and better mechanical performance, but it only works for cylindrical bodies of revolution. It is the process behind ASTM D3299, BS EN 13121 and ASME RTP-1.
Dual laminate: a thermoplastic liner — PP, PVC, PVDF or E-CTFE — overwrapped with structural GRP. It combines the chemical resistance of the pure thermoplastic with the stiffness of the composite, and it is the answer when no polyester or vinyl ester resin will hold the product. It requires certified thermoplastic welding as well as lamination, and it is where manufacturers differ most: many fibreglass shops simply do not offer it.
A manufacturer who commands all three can pick the right one for your application. One who only has filament winding will offer you a cylinder even when you needed a rectangular tank; one who only hand-laminates will overcharge you for a straightforward cylindrical vessel. Ask about all three, and ask as well about the materials available for the shell and the lining.
Why two quotations for the same tank differ by 40 per cent
When you receive three quotations against the same specification and one comes in 40 per cent below the others, the difference is almost never margin. It sits in technical decisions that never appear on the front page of the offer:
The calculated thickness. With no design standard declared, each manufacturer sets the thickness to its own judgement. The same vessel can come out at 8 mm or at 14 mm of wall.
The resin grade. An orthophthalic polyester costs considerably less than an isophthalic, and that in turn less than a vinyl ester or a novolac vinyl ester. If the quotation only says «polyester resin», it says nothing.
The thickness and quality of the corrosion barrier. The first blind spot we have already covered.
The execution of the base-to-shell and top-to-shell joints. The second blind spot: overlay width and thickness, internal as well as external lay-up, and continuity of the corrosion barrier across the seam.
The design factors and the load cases considered. Wind, snow, seismic action, maintenance loads on the roof, ground pressure on buried tanks. Leaving out any one of these load cases makes the vessel cheaper and puts it outside the standard.
The real scope of supply. Manways, nozzles, anchor reinforcement, ladders, handrails, gratings, valves and level instrumentation tend to appear as «as required» in the cheap quotations and come back later as a variation.
Neutralising this is straightforward: require every quotation to state the design standard, the resin by trade name, the corrosion barrier thickness, the structural thickness and the definition of the base-to-shell and top-to-shell joints. With those five figures, comparing offers stops being a lottery.
Eight criteria for assessing a GRP tank manufacturer
Criteria 1 to 3: design standards, resins and experience with your product
Criterion 1 · They design to a standard, and they write it down. A competent manufacturer states in the quotation which standard the laminate has been designed to. If they do not cite one, either they are not calculating or they would rather you could not check. These are the references they should recognise:
| Standard | What it covers | What to ask the manufacturer |
| BS EN 13121 | GRP tanks and vessels for use above ground. Parts 1 to 4: raw materials, composite materials, design and workmanship, and delivery, installation and maintenance. | Do you apply Part 3 to the laminate and joint design? Will you issue the calculations? |
| ASME RTP-1 | US code for reinforced thermoset plastic corrosion-resistant equipment up to 1 barg. Covers design, fabrication, fabricator qualification and inspection. | Do you build to RTP-1? What scope does it cover and who inspects? |
| ASTM D3299 | Filament-wound glass-fibre-reinforced corrosion-resistant tanks. | Do you have filament winding in-house? |
| ASTM D4097 | Contact-moulded glass-fibre-reinforced corrosion-resistant tanks. | What qualification do your laminators hold? |
| BS 4994 | The British standard for the design and construction of vessels in reinforced plastics. Largely superseded by BS EN 13121 but still widely written into UK specifications. | If you cite it, why, and how do you reconcile it with BS EN 13121? |
| PE(S)R 2016 / PED 2014/68/EU | Pressure equipment legislation. Applies above defined pressure and volume thresholds; determines UKCA or CE marking. | What category is the vessel, which conformity module, and which approved body? |
| EPR 2016 and CIRIA C736 | Environmental permitting and secondary containment. Governs bunding, containment capacity and pollution prevention for chemical storage. | Is the tank designed to suit the bund and permit conditions on my site? |
Criterion 2 · They justify the resin rather than just naming it. The resin has to be selected from the stored product, its concentration and its temperature, and the manufacturer should be able to back the choice with the resin supplier’s chemical resistance tables. An orthophthalic will do for water and mild duties; an isophthalic widens the range; a vinyl ester is the standard choice for acids and oxidisers; and a novolac vinyl ester handles severe conditions and higher temperatures. If the product defeats even the novolac, the right answer is a dual laminate with a thermoplastic liner, not «a bit more reinforcement».
Criterion 3 · They have references with your product and your sector, not generic ones. Storing sodium hypochlorite is not the same as storing sulphuric acid, and a tank for a chemical reagent storage installation has little in common with one for process water. Ask for installations equivalent in fluid, concentration, temperature and capacity, with commissioning dates. A manufacturer with real history can show you their own vessels twenty years into service, which is the only genuine proof of durability this product offers.
Criteria 4 to 6: quality control, manufacturing capability and ancillaries
Criterion 4 · They have a quality plan and documented testing. An under-cured laminate is indistinguishable by eye from a sound one, and it fails just as surely as if the wrong resin had been used. These are the checks they should be able to evidence:
| Test / check | What it verifies | Typical acceptance criterion |
| Barcol hardness (ASTM D2583) | Degree of cure of the resin. The most revealing test, and the cheapest. | At least 90 per cent of the value declared by the resin supplier. |
| Wall thickness | That the laminate as built matches the laminate as calculated. | Nominal thickness from the calculations, with no negative tolerance. |
| Glass content (ISO 1172) | Resin-to-glass ratio by loss on ignition. Distinguishes corrosion barrier from structural laminate. | 70-90 per cent resin in the barrier; 30-40 per cent in the structure. |
| Visual inspection for defects | Porosity, air inclusions, dry fibre, crazing, unwetted areas. | BS EN 13121 acceptance criteria, stated in writing. |
| Acoustic emission testing (ASTM E1067) | Structural integrity of the laminate under load: detects delamination, microcracking and internal damage, particularly at the joints. | No significant emission during the stepped load hold. |
| Tightness test | Freedom from leaks before despatch. | Hydrostatic test to full capacity, with a signed record. |
| Spark test | Discontinuities in the liner of dual laminate equipment. | No arcing anywhere across the internal surface. |
Acoustic emission testing deserves a moment. It is the only item on that list that assesses how the laminate behaves under real load rather than at an isolated point: as the tank is filled in steps, sensors pick up the emissions produced by resin microcracking, fibre breakage or interlaminar debonding. It is especially useful exactly where the other tests cannot reach — the base-to-shell and top-to-shell joints — and it works both for accepting a new vessel and for assessing a tank with years of service before deciding whether to repair or replace it.
Criterion 5 · Their manufacturing capability matches what you actually need. There are two limits worth establishing before anything else. The first is capacity: Tecnium builds up to 200,000 litres, alongside vessels, reactors and stacks. The second, and the one that catches people out, is transport: beyond roughly 4 metres in diameter, road haulage becomes complicated and expensive enough to shape the whole project.
Above that threshold there are two routes, and it is worth asking openly which one each supplier offers. Some laminate the tank on site, with the obvious advantage on size and the equally obvious drawback of moving quality control to a location with no controlled temperature, humidity or cleanliness. Tecnium does not build on site: every vessel is laminated entirely in the works, which is where cure, traceability and the full test protocol can be guaranteed. On large-capacity projects, then, the answer is to resolve the sizing at concept stage — splitting the duty across several transportable vessels where that makes sense — rather than discovering the problem once the tank has been designed.
Criterion 6 · They supply the whole package, not just the vessel. An industrial tank is never only a tank: it needs corrosion-resistant valves, level indication, ladders, handrails, gratings and often a cover. When each item comes from a different supplier, dimensional clashes and gaps in responsibility surface during installation. Tecnium also manufactures the valves, gratings, ladders and handrails — including a range of corrosion-resistant valves from DN 25 to DN 1,700 in PP, PVC, PVDF, PTFE and E-CTFE —, so that the whole scope sits with a single party.
Criteria 7 and 8: containment compliance and support through the service life
Criterion 7 · They understand the containment regime, not just the vessel. In the UK, chemical storage sits under the Environmental Permitting Regulations, with secondary containment designed to CIRIA C736, and — where flammable or explosive atmospheres are involved — under DSEAR and, on larger inventories, COMAH. A perfectly built tank can still leave the installation non-compliant if the bund is undersized or the containment detailing has not been considered. What you want from the manufacturer is a vessel designed around those constraints and the documentation your permit application needs. Tecnium routinely delivers installations engineered to a statutory containment regime — in Spain we also draft the APQ-6 legalisation studies and projects that govern corrosive liquid storage — which is the practical evidence that the regulatory side is handled at design stage rather than afterwards.
Criterion 8 · They are still there when the tank is ten years old. BS EN 13121-4 covers precisely delivery, installation and maintenance, and it is the part almost nobody reads. A GRP tank needs periodic inspection of the internal laminate, and when the time comes it can be repaired and re-lined — rebuilding the corrosion barrier from the inside — instead of replaced, provided the attack has not reached the structural laminate. Ask whether the manufacturer offers that service, whether they hold spares for valves and ancillaries, and whether they keep traceability of your vessel. A supplier who only sells new equipment will have you buying another tank when the one you have is perfectly recoverable.
Documentation, procurement mistakes and frequently asked questions
The documentation pack your manufacturer should hand over
A competent GRP tank manufacturer hands over, without being chased, a file that stays with the vessel for its whole service life. Write it into the specification, not into the handover meeting:
Design calculations for the laminate and the joints, with the standard applied, the load cases and the design factors.
Fabrication drawings showing manways, nozzles, reinforcement, anchorage and the detail of the base-to-shell and top-to-shell joints.
Laminate schedule layer by layer: veil, corrosion barrier and structure, with thicknesses and weights.
Raw material certificates for resin and reinforcement, with batch numbers and dates.
Signed test records: Barcol, thicknesses, tightness, visual inspection and acoustic emission where contracted.
Declaration of conformity and marking, including the pressure equipment documentation where the vessel operates under pressure.
Installation, operating and maintenance manual with the recommended inspection programme.
You can gauge the level of detail you should expect from the technical documentation for plastic and GRP tanks we publish openly.
Five common mistakes when buying a GRP tank
Comparing quotations on price and capacity. Without the standard, the resin, the barrier thickness and the joint definition declared, you are not comparing the same product.
Specifying the product without concentration or temperature. «Sulphuric acid» does not define a resin. At 30 per cent and at 96 per cent these are different projects.
Forgetting the site load cases. Wind, snow and seismic action change the calculation, and it is the buyer’s job to state them correctly in the specification.
Leaving containment and permitting until later. Bunding requirements drive the location and the layout, and discovering that once the tank is built is expensive.
Not planning access and installation. Headroom, crane access and manoeuvring space decide whether the tank can arrive in one piece or the duty has to be split across several vessels.
Frequently asked questions about GRP tank manufacturers
Frequently asked questions
As a minimum, five things in writing in the quotation: the design standard applied, the resin identified by trade name, the corrosion barrier thickness, the structural laminate thickness, and the definition of the joints between the base, the top and the shell. Add references with your own product and concentration, the test plan they intend to carry out, and the exact scope of supply including ancillaries. With that, you can compare offers on a like-for-like basis; without it, you are only comparing price.
From the testing, not from the appearance. Barcol hardness shows whether the resin has fully cured, wall thickness confirms that what was calculated is what was built, and loss on ignition verifies the resin-to-glass ratio in each zone of the laminate. For structural integrity under load — and particularly at the joints — the appropriate test is acoustic emission. Add visual inspection against the BS EN 13121 defect criteria and a tightness test before despatch. A manufacturer who does not hand over that signed protocol is evidencing nothing.
Because the base, the shell and the top are built separately and joined afterwards with an overlay laminate, so the seam accumulates the highest mechanical loading on the tank and the most vulnerable point of the corrosion barrier. The base-to-shell joint carries the full hydrostatic load plus the bending from the change in geometry; and if the internal overlay does not rebuild the barrier with the same veil and the same resin content, the seam leaves structural laminate exposed to the product. Ask about the width and thickness of the overlay, whether it is applied inside as well as outside, how the surfaces were prepared, and what knuckle radius the transition has.
A dual laminate is a thermoplastic inner liner — PP, PVC, PVDF or E-CTFE — overwrapped with structural GRP. You go to it when no polyester or vinyl ester resin will hold the product: strongly oxidising acids, solvents, elevated temperatures or purity requirements. It delivers the chemical resistance of the pure thermoplastic with the stiffness of the composite. It requires thermoplastic welding in addition to lamination, so not every fibreglass fabricator can offer it.
In most cases it can be repaired. Where the chemical attack has been confined to the corrosion barrier and has not reached the structural laminate, the vessel can be re-lined internally: the damaged layer is removed and the veil and barrier rebuilt. Cracks, nozzles and manways can also be repaired locally. Replacement only becomes unavoidable with generalised delamination in the structure — something acoustic emission testing can establish before you commit either way. Which is why it matters that the manufacturer keeps traceability of the vessel and offers inspection and repair.
They are not obliged to, but a manufacturer who engages with it saves you the most common problem on these projects. Chemical storage in the UK falls under environmental permitting, with secondary containment designed to CIRIA C736, and under DSEAR where flammable atmospheres arise. When the equipment supplier and the consultant handling compliance are different parties, it is common for neither to own the interface requirements — bund capacity, nozzle positions, access for inspection. Agree at tender stage who is responsible for what.
If you are assessing GRP tank manufacturers for a specific project, the Tecnium technical team can review your specification, propose the optimal construction — GRP, thermoplastic or dual laminate — and supply the complete technical file. Request a no-obligation quotation and get advice from a manufacturer with more than 70 years of experience in corrosion-resistant equipment for the chemical industry, water treatment, surface treatment and fertiliser production.
How can we help you?
Tell us about your application and we will advise you the most optimal solution to solve your needs of gas treatment, odor control and storage and pumping of corrosive fluids.